Explore our elite range of world-class molecular sieves, silica gels, and activated aluminas engineered for extreme industrial performance.
Pioneering excellence in chemical adsorption manufacturing since 1994 with rigorous quality control and technical innovation.
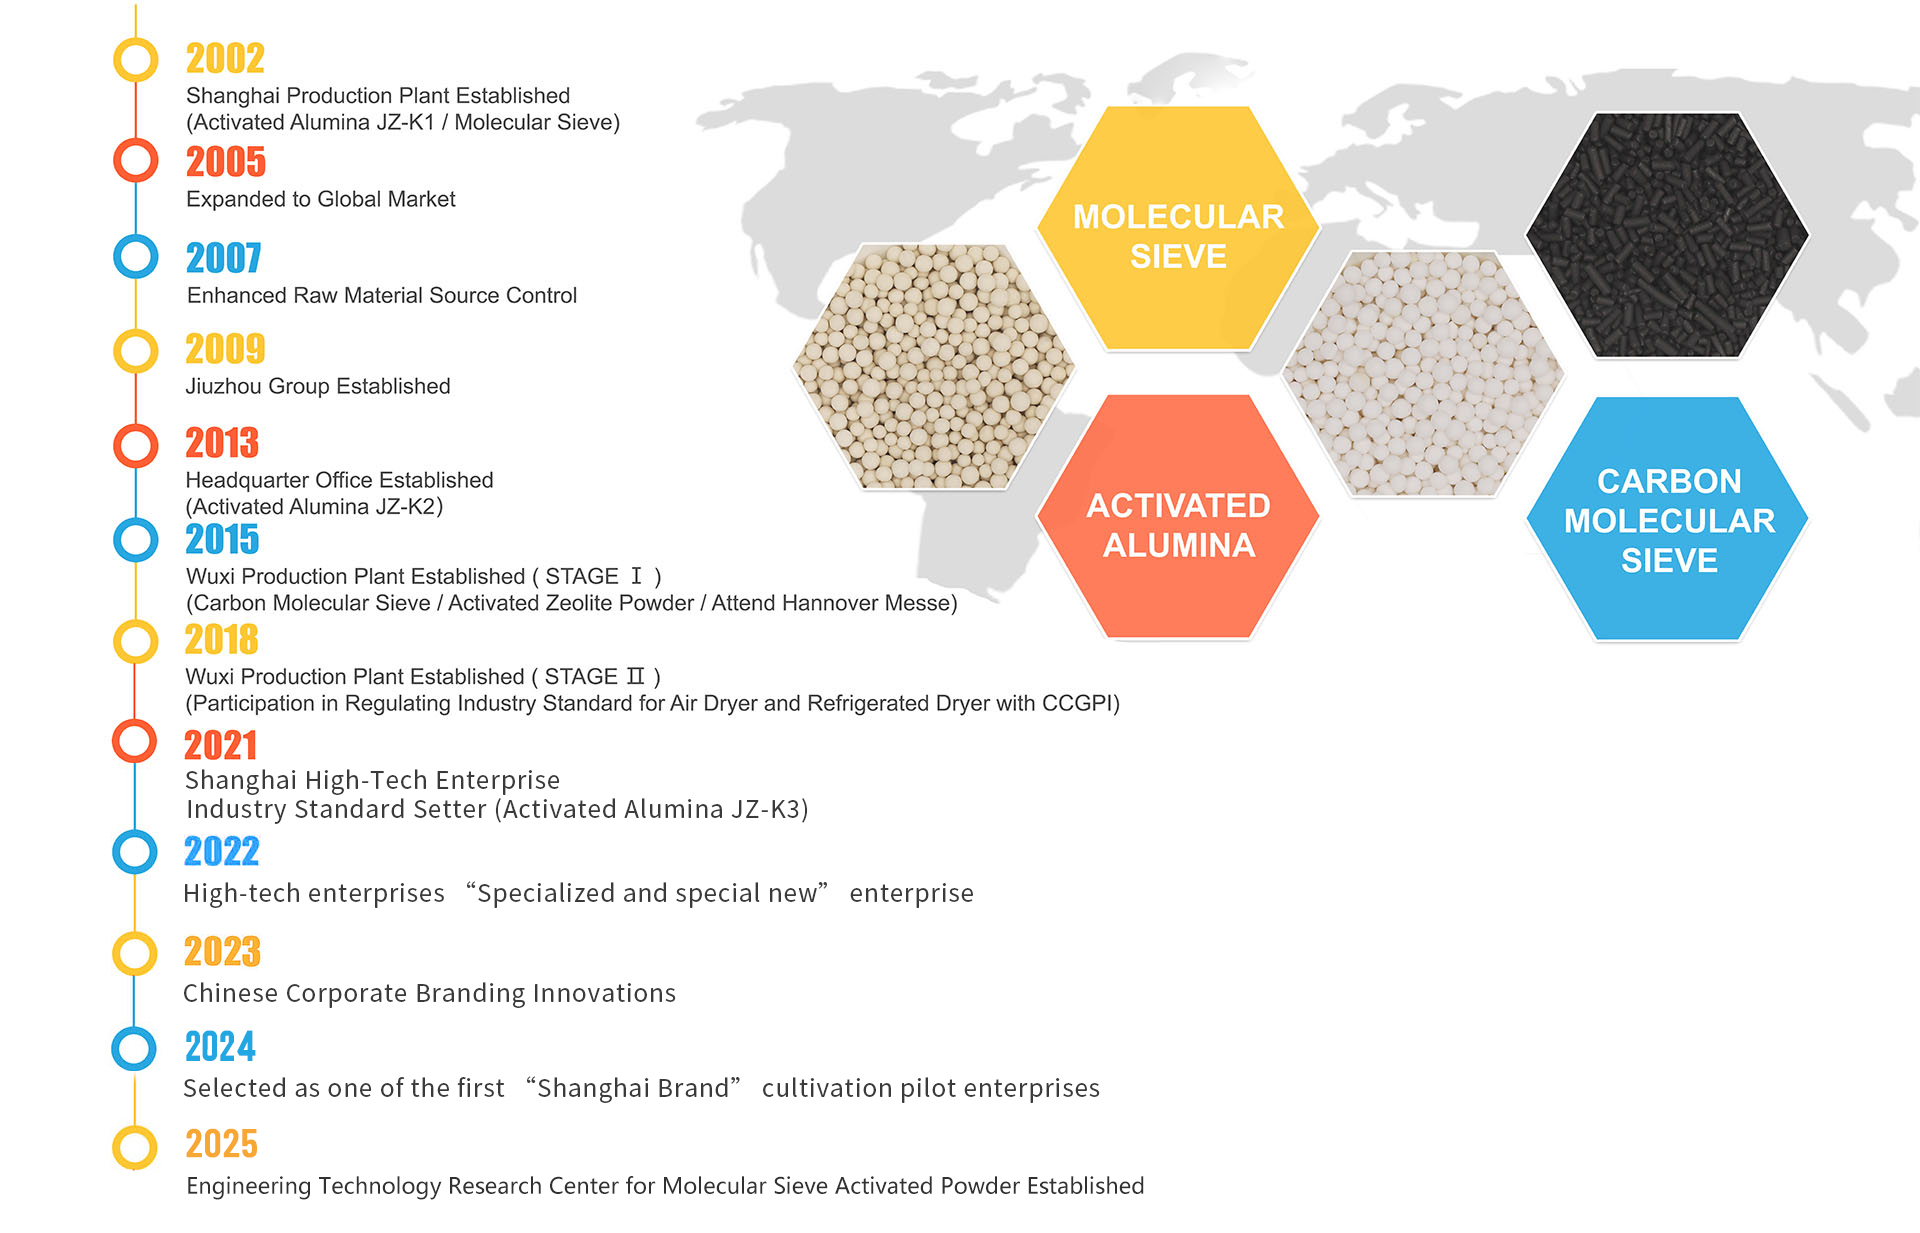
Shanghai Jiuzhou Chemicals Co., Ltd. Located in the biggest Economic Development city Shanghai. Over the years Jiuzhou has always adhered to the “quality control, innovation “principles, committed to the development, research, manufacturing of high quality innovative chemical products. Our main products includes various molecular sieve powders, molecular sieves, activated powder, activated alumina, aluminum oxide catalysts, different types of alumina packing and ceramic balls, sodium silicates, aluminum hydroxide,zeolite 4A, sodium carbonates, SLES, etc. Our all products passed the ISO9001: 2008 quality management system certification and TUV & SGS Certification.
Jiuzhou factory has a professional and world-class research team and experts in chemical product resources. We use the best in international production technology and professional production equipment, constructed in line with national standards and by the large multipurpose plant monitoring, analysis instrument composition the central laboratory. And in quality inspection aspect Jiuzhou have controlled and that products meet international standards.
Jiuzhou's technical strength and industry reputation are leading the industry in the field of desiccants, with senior experts and technical reserves, automated multi-unctional production workshops, and a central laboratory and dynamic laboratory composed of large-scale monitoring and analysis instruments. It is in quality control And in terms of supporting services, a set of scientific and complete operating system has been established Joozeo products are exported to all parts of the world, and have established a distribution network in the United States, Southeast Asia, Japan, Europe, North and South America, the Middle East and other places to provide partners with high-quality products, customized services, and more energy-saving and environmentally friendly adsorption solutions.
Discover high-purity oxygen molecular sieves, soda ash, ceramic balls, and advanced custom chemical formulations.
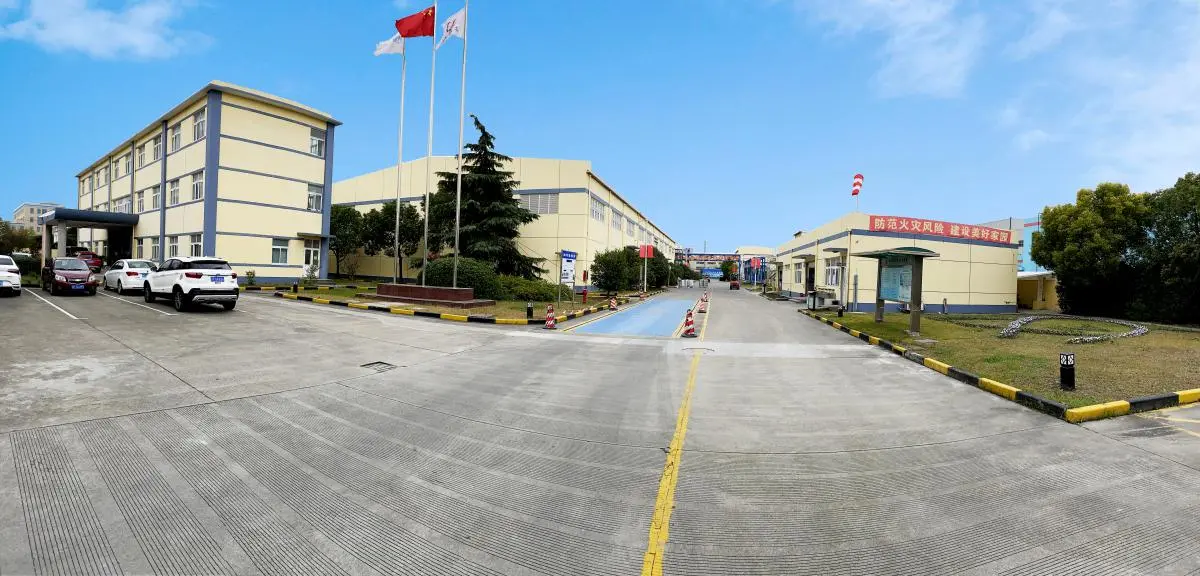
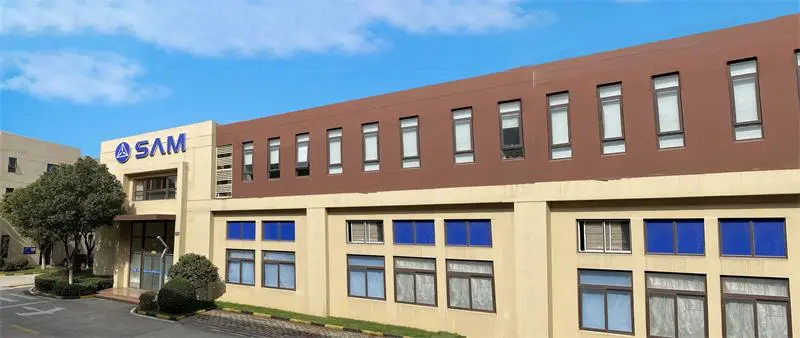
State-of-the-art production plants equipped with automated workflows and precision laboratory instrumentation.
Built on an unyielding dedication to immaculate quality and continuous chemical engineering innovation.
Rigorous multi-stage batch inspection protocols ensuring absolute reliability under high-pressure industrial cycles.
Continuous R&D investment in high-efficiency adsorption media, green catalysts, and energy-saving desiccants.
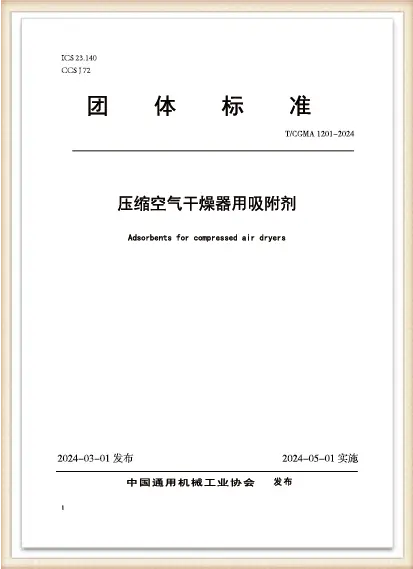
As an industry authority, Jiuzhou has actively drafted and contributed to numerous national and industrial technical standards.
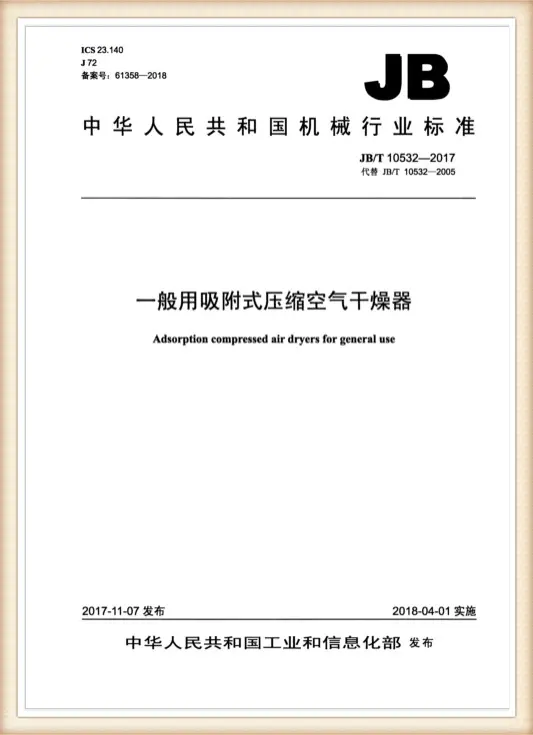
JB / T 10532-2017
Adsorption compressed air dryers for general use
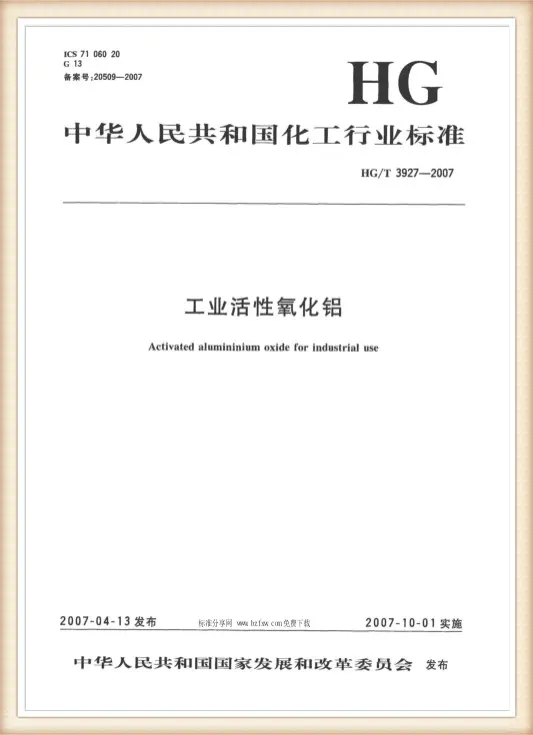
HG / T 3927-2007
Activated aluminum oxide for industrial use
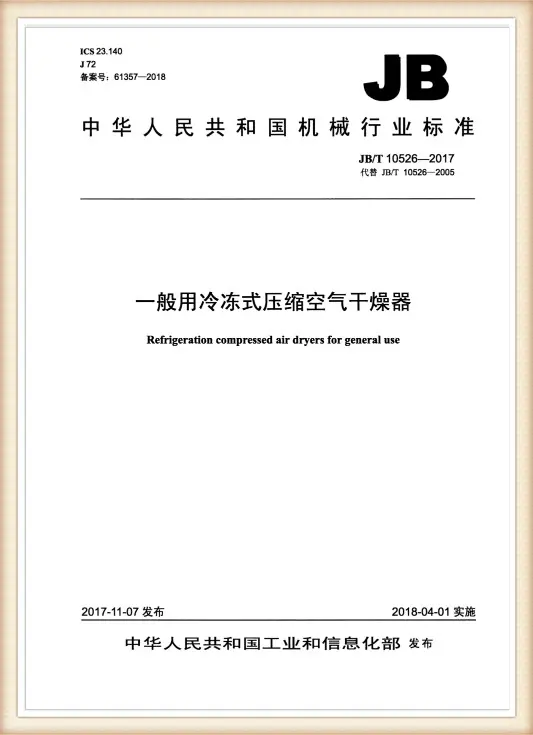
JB / T 10526-2017
Refrigeration compressed air dryers for general use
T/CGMA1201-2024
Advanced Industrial Gas Standards
T/HGHX 02—2024
Environmental Adsorption Spec
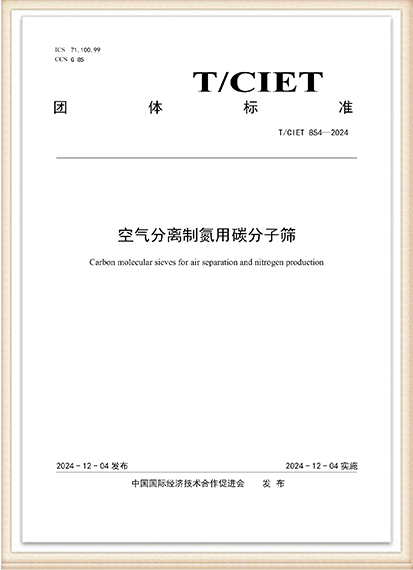
T/CIET 854-2024
High-Tech Material Quality Benchmark
Deep dive into next-generation molecular sieve architectures and global industrial deployment strategies.
The global adsorption industry is undergoing a paradigm shift driven by stringent decarbonization targets and extreme-purity gas separation requirements. Molecular sieves (zeolites) and specialized desiccants are transitioning from macro-porous structures to hierarchically structured nano-composite frameworks. These next-generation products offer enhanced mass transfer kinetics, lower regeneration energy consumption, and superior thermal hydrothermal stability.
Looking toward 2030, our R&D roadmap focuses on carbon capture utilization and storage (CCUS) grade carbon molecular sieves (CMS), hydrogen purification pressure swing adsorption (PSA) media, and intelligent self-indicating desiccants integrated with IoT sensor systems. By optimizing crystal pore dimensions at the angstrom level, Jiuzhou empowers petrochemical, cryogenic air separation, and pharmaceutical plants to achieve unprecedented purity thresholds.
Industrial ecosystems demand holistic adsorption solutions rather than isolated chemical supplies. Jiuzhou delivers turnkey macro-solutions encompassing air compressor drying, petrochemical sweetening, insulated glass dew point control, and medical oxygen concentration. By combining customized particle grading, optimized bed packing geometry, and dynamic computer simulation modeling, we minimize pressure drops while maximizing lifecycle adsorption capacity for mega-scale industrial facilities.
Unmatched manufacturing resilience, strict international regulatory alignment, and localization support.
Integrating Industry 4.0 paradigms into chemical manufacturing, our automated multi-functional workshops leverage real-time distributed control systems (DCS), AI-driven batch monitoring, and automated packaging lines. This digital transformation guarantees absolute batch-to-batch consistency, drastically reduced lead times, and robust supply chain resilience even amidst global logistics turbulence.
Navigating complex international trade frameworks requires rigorous compliance. All Jiuzhou products adhere strictly to ISO9001, TUV, SGS, REACH, and RoHS standards. Through our established distribution network across North America, Europe, Southeast Asia, and the Middle East, we provide localized technical support, custom formulation engineering, and rapid on-site troubleshooting.
Our solemn commitment to ecological sustainability, green chemistry, and clean atmospheric environments.
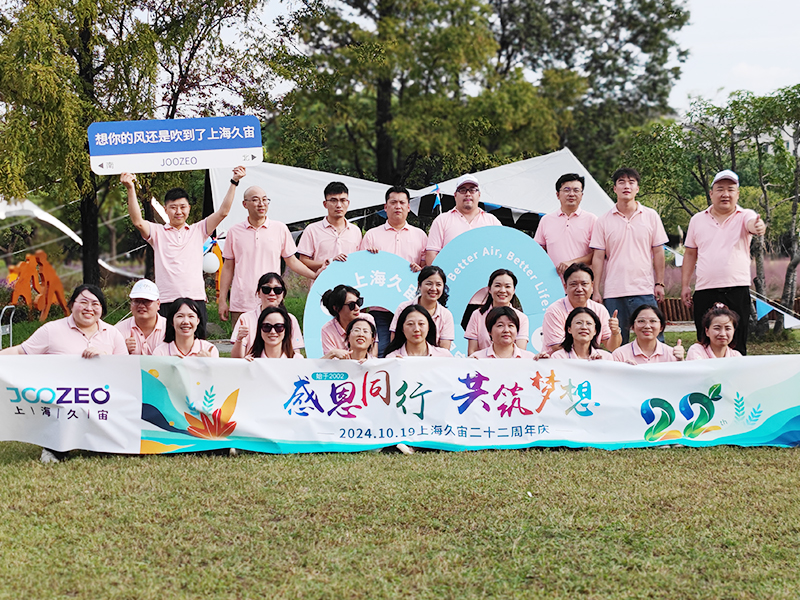
“Better air, Better life”
Expert answers regarding procurement, technical specifications, and custom manufacturing capabilities.
A: Our molecular sieves feature high crushing strength, low attrition rates, precise pore size distribution (e.g., 3A, 4A, 5A, 13X), and exceptional hydrothermal stability, ensuring extended service intervals in heavy-duty PSA and TSA units.
A: Yes. With our state-of-the-art central laboratories and senior chemical engineers, we offer bespoke formulations, particle size adjustments, and custom activation profiles tailored to unique client specifications.
A: All our manufacturing facilities and products are fully certified under ISO9001:2008 quality management systems, TUV, SGS, and comply with strict global environmental and safety mandates including REACH.
A: Operating across expansive manufacturing bases in Shanghai and Wuxi, combined with automated 4.0 production lines and robust international distribution hubs, we guarantee stable stock levels and efficient global logistics.
Any Problem, please feel free to contact us. Respond within 24 hours with expert technical consultation and competitive pricing.
Send Request & Inquire Now