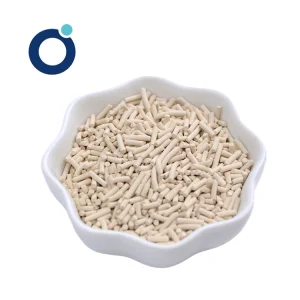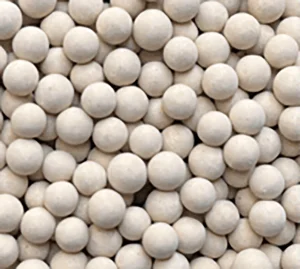
As industry leaders, we understand the critical role of Active Alumina Powder in petrochemical refining, air separation, and water treatment. Our research-driven approach ensures that our products provide unmatched adsorption kinetics and thermal stability.
Global procurement teams demand more than just competitive pricing; they require supply chain security and technical transparency. Our manufacturing facilities in Shanghai and Wuxi operate under strict ISO9001:2008 standards, ensuring that every batch meets the complex requirements of global industrial players.
The chemical industry is shifting towards "Green Adsorption." Our roadmap focuses on increasing the surface area-to-volume ratio of alumina particles to enhance catalytic efficiency, significantly reducing energy consumption for our partners in North America, Europe, and Asia.
We pride ourselves on being a Standard Setter. By strictly adhering to JB/T 10532 and HG/T 3927 standards, we provide the technical documentation required for smooth customs clearance and regulatory compliance across 80+ countries.
A: We utilize centralized laboratories equipped with automated monitoring and analysis systems, ensuring 100% adherence to international quality protocols.
A: Yes, our R&D team specializes in tailoring adsorption solutions to specific industrial applications, ranging from gas drying to catalyst support.